Carbide drill bits
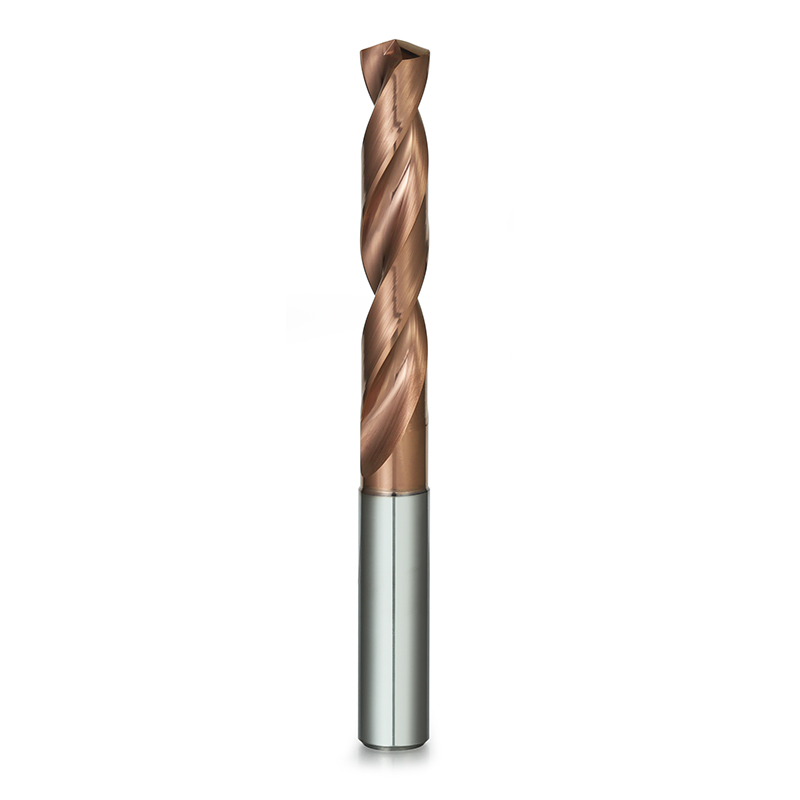
KERNVEX External Cooling 2 Flutes Drills
Range reference: KVX-001
- workpiece material
- Soft steel; Hardened and tempered steel; Tempering stainless steel; Cast iron; Bearing steel; Deep hole working
- application type
- Drilling
- Coating
- Self development comparable to DR coating
• Material: MG-grade carbide rods,ultra-fine grain size 0.8um,10% Coblat • Coating: Self-develped coating (benchmarking B-a-l-z-a-s DR Coating) • Coating hardness: 2000-4000HV • Ultra-low friction coefficient:0.05-0.15 • Helix angle: 30° • Point angle:138.9° • Large rake angle: 16° • Negative chamfer: -6° • Variable core thickness: 30–40% • Variable outer diameter: 0.8°
Enquire about this tool →Technical data
| Product Name | External Coolant Drill Bit |
| Material | Solid carbide |
| Process | Fully Gorund (Roll Forged & Polished, Roll Forged, Milled are Available) |
| Size | Standard size or as request |
| Point Type | 118 Degree Regular Point (1-3mm); 138 Degree Split Point(3-20mm) |
| Shank Type | Straight Shank (Tree Flats Shank, 1/2" Shank Sliver & Deming, Reduced Shank,1/4" Quick Change Hex Shank are Available) |
| Surface Finish | Amber Color (Bright, Black Oxide, Titanium, Black & Gold, are Available) |
| Package | Plastic Box or as request |
Additional technical data
| Product Code | Blade diameter | Blade Length H | Full L | Shank D | ||||||
| 3XD | 5XD | 8XD | 3XD | 5XD | 8XD | 3XD | 5XD | 8XD | ||
| EXWL00400 | 4 | 24 | 36 | 43 | 66 | 74 | 81 | 6 | 6 | 6 |
| EXWL00450 | 4.5 | 24 | 36 | 43 | 66 | 74 | 81 | 6 | 6 | 6 |
| EXWL00500 | 5 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXWL00550 | 5.5 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXWL00600 | 6 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXWL00650 | 6.5 | 34 | 53 | 76 | 79 | 91 | 114 | 8 | 8 | 8 |
| EXWL00700 | 7 | 34 | 53 | 76 | 79 | 91 | 114 | 8 | 8 | 8 |
| EXWL00750 | 7.5 | 41 | 53 | 76 | 79 | 91 | 116 | 8 | 8 | 8 |
| EXWL00800 | 8 | 41 | 53 | 76 | 79 | 91 | 116 | 8 | 8 | 8 |
| EXWL00850 | 8.5 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXWL00P00 | 9 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXWL00950 | 9.5 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXWL01000 | 10 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXWL01050 | 10.5 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXWL01100 | 11 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXWL01150 | 11.5 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXWL01200 | 12 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXWL01250 | 12.5 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXWL01300 | 13 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXWL01350 | 13.5 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXWL01400 | 14 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXWL01450 | 14.5 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXWL01500 | 15 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXWL01550 | 15.5 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXWL01800 | 16 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXWL01850 | 16.5 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXWL01700 | 17 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXWL01750 | 17.5 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXWL01800 | 18 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXWL01850 | 18.5 | 79 | 101 | 131 | 153 | 20 | 20 | 20 | ||
| EXWL01900 | 19 | 79 | 101 | 131 | 153 | 20 | 20 | 20 | ||
| EXWL01950 | 19.5 | 79 | 101 | 131 | 153 | 20 | 20 | 20 | ||
| EXWL02000 | 20 | 79 | 101 | 131 | 153 | 20 | 20 | 20 | ||
Technical notes
- This external coolant solid carbide drill is designed for stable and efficient drilling in steel and general metal applications.
- Ideal for ≤ 3×D drilling , standard CNC machines, and applications without internal coolant supply.
- 1. Premium Carbide Substrate
- • Manufactured from imported MG-grade carbide rods
- • Ultra-fine grain size: 0.8 μm
- • 10% cobalt content for excellent toughness and wear resistance
- • Suitable for high-speed and stable drilling in steel materials
- This substrate provides a good balance between hardness and toughness, ensuring consistent performance under general machining conditions.
- (Benchmarking Balzers DR Coating)
- • Independently developed coating with in-house coating equipment
- • Optimized for steel and general-purpose drilling
- • Coating hardness: 2000–4000 HV
- • Low friction coefficient: 0.05–0.15
- • Effectively reduces:
- • Built-up edge
- • Surface scratching
- The coating ensures smooth chip flow and extended tool life in continuous production.
- 3. Optimized Drill Geometry for External Coolant
- • Point angle: 138.9°
- • Double cutting edge design improves:
- • Cutting stability
- • Wear resistance
- • Equalized web design reduces drill wandering and improves hole accuracy
- • Optimized for external coolant or dry-assisted machining
- This geometry provides reliable performance in standard drilling operations.
- 4. Efficient Flute & Core Design
- This design improves cutting smoothness and chip evacuation, especially in shallow and medium-depth holes.
- 5. Application Materials
- Suitable for drilling:
- • Quenched and tempered steel
- • Quenched and tempered stainless steel
- • Bearing steel
- Recommended for general-purpose drilling and standard production environments .
- To ensure stable performance, long tool life, and consistent quality, every external coolant carbide drill is produced under a fully controlled manufacturing and inspection system.
- Precision Edge Preparation Technology
- • Drill tips are manually edge-honed and chamfered to improve edge strength and reduce micro-chipping
- • Final edge preparation completed by fully automatic passivation equipment
- • Rubber-bonded diamond abrasive polishing process ensures uniform edge radius on all cutting edges
- • Edge passivation tolerance strictly controlled within ±0.003 mm
- • Optimized edge preparation improves:
- • Tool life in continuous production
- Advanced Manufacturing Equipment
- • High-precision grinding ensures:
- • Accurate drill geometry
- • Sharp and consistent cutting edges
- • Smooth and stable drilling performance
- • In-house grinding capability allows flexible production and OEM customization
- Strict Quality Inspection & Control
- • Profile accuracy and corner radius controlled within 3 μm
- • 100% visual inspection at 300× magnification
- • No edge chipping
- • No serrations
- • No surface defects
- • In-house coating machines ensure full control over:
- • Coating thickness consistency
- • Adhesion reliability
- • Batch-to-batch stability
- • Integrated inspection system guarantees consistent quality from raw material to finished product
- Helix angle: 30°
- Large rake angle: 16°
- Negative chamfer: -6°
- Variable core thickness: 30–40%
- Variable outer diameter: 0.8°