Carbide drill bits
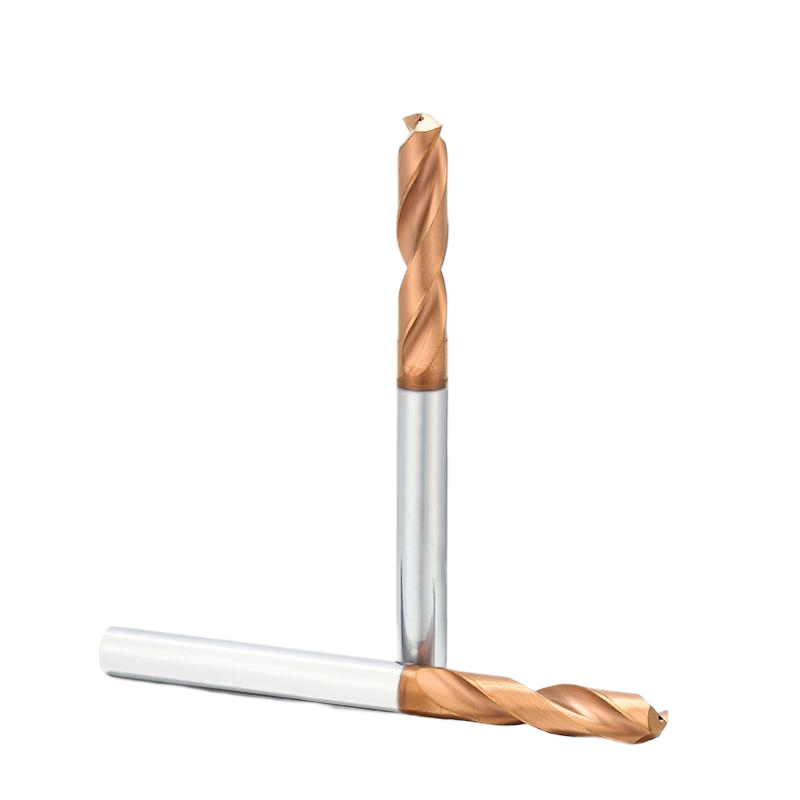
KERNVEX Interal Cooling 2 Flutes High Speed Drills
Range reference: KVX-005
- workpiece material
- Soft steel; Hardened and tempered steel; Tempering stainless steel; Cast iron; Bearing steel; Deep hole working
- application type
- Drilling
- Coating
- Self development comparable to DR coating
• Material: MG-grade carbide rods,ultra-fine grain size 0.8um,10% Coblat • Coating: Self-develped coating (benchmarking B-a-l-z-a-s DR Coating) • Coating hardness: 2000-4000HV • Ultra-low friction coefficient:0.05-0.15 • Helix angle: 30° • Point angle:138.9° • Large rake angle: 16° • Negative chamfer: -6° • Variable core thickness: 30–40% • Variable outer diameter: 0.8°
Enquire about this tool →Technical data
| Product Name | Internal Coolant Drill Bit |
| Material | Solid carbide |
| Process | Fully Gorund (Roll Forged & Polished, Roll Forged, Milled are Available) |
| Size | Standard size or as request |
| Point Type | 118 Degree Regular Point (1-3mm); 138 Degree Split Point(3-20mm) |
| Shank Type | Straight Shank (Tree Flats Shank, 1/2" Shank Sliver & Deming, Reduced Shank,1/4" Quick Change Hex Shank are Available) |
| Surface Finish | Amber Color (Bright, Black Oxide, Titanium, Black & Gold, are Available) |
| Package | Plastic Box or as request |
Additional technical data
| Product Code | Blade diameter | Blade Length H | Full L | Shank D | ||||||
| 3XD | 5XD | 8XD | 3XD | 5XD | 8XD | 3XD | 5XD | 8XD | ||
| EXNJ00400 | 4 | 24 | 36 | 43 | 66 | 74 | 81 | 6 | 6 | 6 |
| EXNJ00450 | 4.5 | 24 | 36 | 43 | 66 | 74 | 81 | 6 | 6 | 6 |
| EXNJ00500 | 5 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXNJ00550 | 5.5 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXNJ00600 | 6 | 28 | 44 | 57 | 66 | 82 | 95 | 6 | 6 | 6 |
| EXNJ00650 | 6.5 | 34 | 53 | 76 | 79 | 91 | 114 | 8 | 8 | 8 |
| EXNJ00700 | 7 | 34 | 53 | 76 | 79 | 91 | 114 | 8 | 8 | 8 |
| EXNJ00750 | 7.5 | 41 | 53 | 76 | 79 | 91 | 116 | 8 | 8 | 8 |
| EXNJ00800 | 8 | 41 | 53 | 76 | 79 | 91 | 116 | 8 | 8 | 8 |
| EXNJ00850 | 8.5 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXNJ00P00 | 9 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXNJ00950 | 9.5 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXNJ01000 | 10 | 47 | 61 | 95 | 89 | 103 | 142 | 10 | 10 | 10 |
| EXNJ01050 | 10.5 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXNJ01100 | 11 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXNJ01150 | 11.5 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXNJ01200 | 12 | 55 | 71 | 114 | 102 | 118 | 162 | 12 | 12 | 12 |
| EXNJ01250 | 12.5 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXNJ01300 | 13 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXNJ01350 | 13.5 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXNJ01400 | 14 | 60 | 77 | 133 | 107 | 124 | 178 | 14 | 14 | 14 |
| EXNJ01450 | 14.5 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXNJ01500 | 15 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXNJ01550 | 15.5 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXNJ01800 | 16 | 65 | 83 | 152 | 115 | 133 | 204 | 16 | 16 | 16 |
| EXNJ01850 | 16.5 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXNJ01700 | 17 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXNJ01750 | 17.5 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXNJ01800 | 18 | 73 | 93 | 171 | 123 | 143 | 223 | 18 | 18 | 18 |
| EXNJ01850 | 18.5 | 79 | 101 | - | 131 | 153 | - | 20 | 20 | 20 |
| EXNJ01900 | 19 | 79 | 101 | - | 131 | 153 | - | 20 | 20 | 20 |
| EXNJ01950 | 19.5 | 79 | 101 | - | 131 | 153 | - | 20 | 20 | 20 |
| EXNJ02000 | 20 | 79 | 101 | - | 131 | 153 | - | 20 | 20 | 20 |
Additional technical data
| Item | Internal Coolant Drill | External Coolant Drill |
| Coolant Supply | Coolant flows through internal channels directly to the cutting edge | Coolant supplied externally by machine nozzles |
| Visual Apperance | Visible coolant holes on the drill body | Solid body, no visible holes |
| Chip Evacuation | Excellent | Limited |
| Suitable Drillling Depth | 5XD,8XD,12XD,up to 30XD | Typically≤3XD |
| Cutting Stability | Very high, minimal vibration | Reduced stability in deep holes |
| Cooling Efficiency | Direct cooling at cutting zone | Cooling easily blocked by chips |
| Machine Requirement | Must support internal coolant | Standard machines supported |
Technical notes
- This internal coolant solid carbide drill is designed for high-efficiency deep hole drilling and demanding cutting conditions.
- Ideal for deep hole machining, high-speed cutting, and difficult-to-machine materials.
- 1. Premium Carbide Substrate
- • Made from imported MG-grade carbide rods
- • Ultra-fine grain size: 0.8μm
- • 10% cobalt content for balanced toughness and wear resistance
- • Excellent adaptability to high-speed and high-feed drilling
- This substrate ensures strong edge stability while maintaining sharpness during long cutting cycles.
- (Benchmarking B-a-l-z-a-s DR Coating)
- • Proprietary coating independently developed in-house
- • After edge passivation post-treatment
- • Coating hardness: 2000–4000 HV
- • Ultra-low friction coefficient: 0.05–0.15
- • Significantly reduces:
- • Edge chipping
- • Adhesion and scratching
- The coating effectively extends tool life and ensures stable performance in continuous deep hole drilling.
- 3. Optimized Drill Geometry Design
- Advanced Point & Cutting Edge Design
- • Point angle: 138.9°
- • Double cutting lip design:
- • Primary cutting edge ensures cutting efficiency
- • Secondary cutting edge improves wear resistance and chip breaking
- • Equalized web design with angular offset
- • Forms a chip-splitting point structure
- • Prevents drill wandering
- • Enables fast material engagement and stable positioning
- This geometry allows smooth cutting and precise hole accuracy even in deep drilling applications.
- 4. High-Efficiency Flute & Core Design
- This flute structure significantly improves:
- • Chip evacuation
- • Cutting stability
- • Tool rigidity during deep hole drilling
- 5. Wide Application Range
- Suitable for machining:
- • Quenched & tempered steel
- • Quenched & tempered stainless steel
- • Bearing steel
- • Deep hole drilling applications
- Technical Comarison
- How to Choose the Right Drill?
- ✔ Choose an Internal Coolant Drill when:
- • Drilling depth is ≥ 5×D
- • Machining stainless steel or alloy steel
- • High requirements for tool life and hole accuracy
- • High-speed, continuous CNC production
- ✔ Choose an External Coolant Drill when:
- • Drilling depth is ≤ 3×D
- • Machining aluminum or mild steel
- • Machine does not support internal coolant
- • Cost-sensitive applications
- 2.Self-Developed High-Performance Coating
- Helix angle: 30°
- Large rake angle: 16°
- Negative chamfer: -6°
- Variable core thickness: 30–40%
- Variable outer diameter: 0.8°