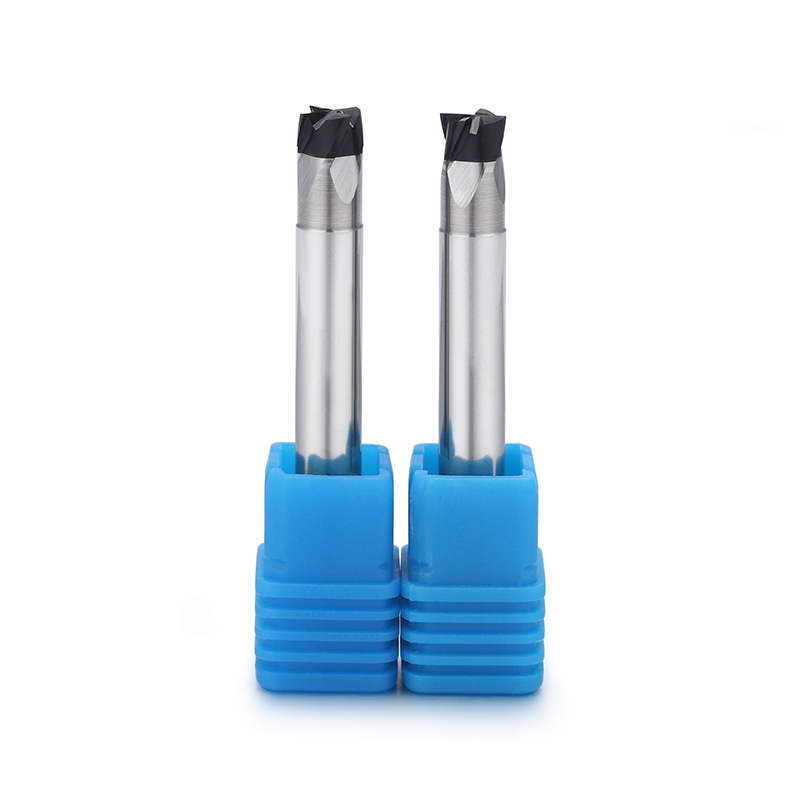
CBN End mill for quenched steel
CBN Square End Mill for HRC60+ Hardened Steel Finishing
Range reference: KVX-007
- workpiece material
- Hardened steel
- application type
- Finishing; medium
- flute type
- Square
• Material: Self-developed NL900 • Grain Size:1.0um • Hardness:HV4100+ • Machining: Hrc60+ hardened steel • Design: 70% large core diamater, 20° helix angle, 10° negative charmfer edge • Tool Life: Up to 20 hours
Enquire about this tool →Technical data
| Item | Details |
| Name | CBN square end mill |
| Material | Self-developed NL900 |
| Grain Size | 1.0μm |
| Hardness | HV4100+ |
| Suitable Workpiece Hardness | HRC60+ |
| Helix Angle | 20° |
| Core Diameter Design | 70% Large Core Diameter |
| Edge Treatment | 10° Negative Chamfer |
| Brazing Method | Vacuum Brazing |
Additional technical data
| Machining Need | Why Choose CBN Square End Mill |
|---|---|
| Flat surface finishing | Provides stable flat-bottom machining and surface consistency |
| Bottom surface finishing | Suitable for mold bottoms, pockets, and flat hardened areas |
| Step face machining | Helps maintain clear step geometry and dimensional accuracy |
| Sharp corner finishing | Suitable when a clear corner edge is required |
| Straight side-wall finishing | Supports stable finishing of vertical surfaces |
| Precision insert machining | Suitable for small hardened components and mold inserts |
| Batch finishing | CBN material helps maintain tool life and dimensional consistency |
Technical notes
- The KERNVEX CBN square end mill is designed for HRC60+ hardened steel finishing, quenched steel machining, and precision mold finishing applications.
- Unlike a CBN ball nose end mill, which is mainly used for 3D curved surfaces and mold cavity contours, a CBN square end mill is more suitable for flat surface finishing, bottom surface finishing, step face machining, straight side walls, and sharp corner finishing.
- Compared with a CBN corner radius end mill, the square end mill provides a sharper cutting corner and better control when a flat bottom, clear edge, or precise step profile is required.
- This tool is suitable for hardened mold steel, die steel, quenched steel parts, precision inserts, flat mold areas, step faces, sharp corners, and high-hardness components where dimensional stability and surface consistency are important.
- CBN tools are not always used to replace carbide in every condition. They are more suitable when the workpiece hardness, finishing allowance, machine rigidity, toolpath stability, and surface finish requirement match CBN machining conditions. For a broader comparison, see When Should You Use a CBN End Mill Instead of Carbide?
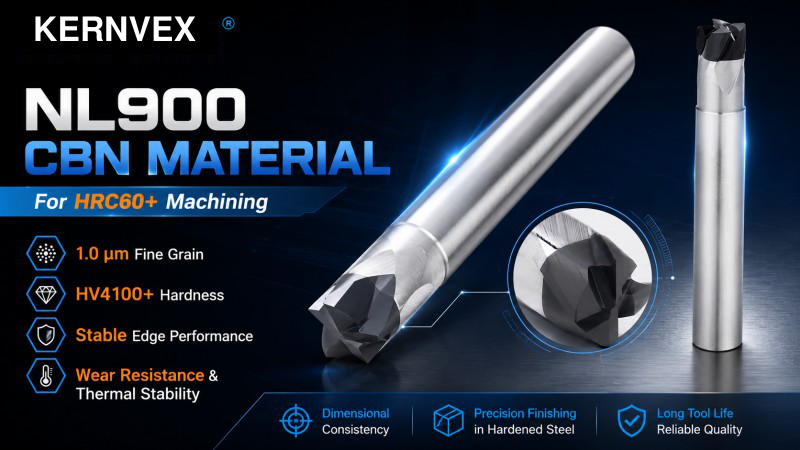
- NL900 CBN Material for HRC60+ Machining
- The 1.0 μm fine grain structure and HV4100+ hardness help improve edge stability, wear resistance, and thermal stability during high-hardness steel finishing. This supports better dimensional consistency and longer cutting performance in continuous precision machining.
- The tool uses a vacuum brazing process to improve bonding stability between the CBN cutting part and the tool body. Compared with ordinary brazing, vacuum brazing helps reduce oxidation, reduce insert deformation, and improve bonding strength.
- For HRC60+ hardened steel finishing, stable CBN edge bonding is important because cutting force, cutting heat, vibration, and long-cycle finishing can directly affect tool life and surface finish.
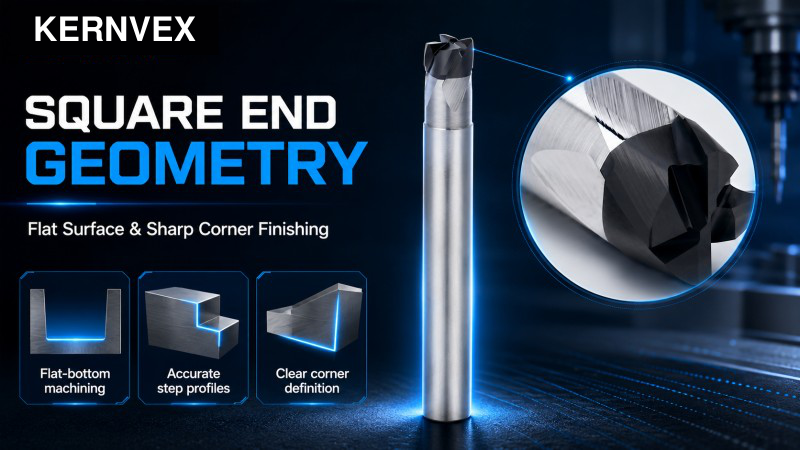
- Square End Geometry for Flat Surface and Sharp Corner Finishing
- The square end geometry is designed for flat surface finishing, bottom surface finishing, step face machining, and sharp corner finishing.
- This makes the tool especially useful when the workpiece requires clear corner definition, accurate step profiles, and stable flat-bottom machining after heat treatment.
- For users comparing CBN square, ball nose, and corner radius tools, this guide explains the selection logic more clearly: CBN End Mill for Hardened Steel: Square vs Ball Nose vs Corner Radius
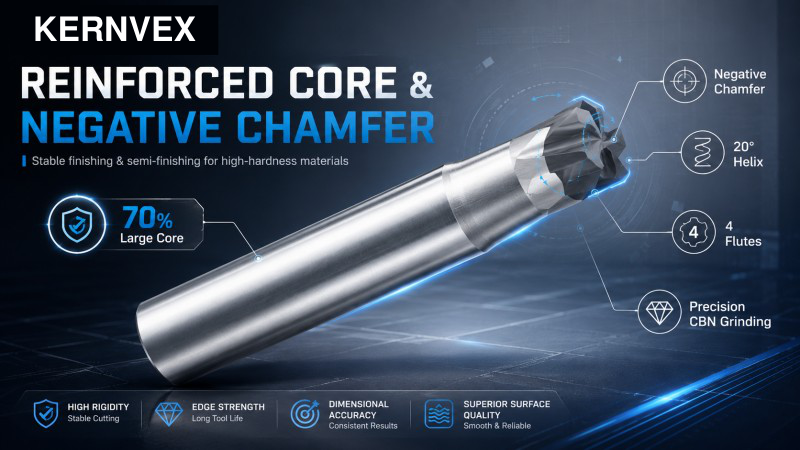
- Reinforced Core and Negative Chamfer Edge
- The tool adopts a reinforced geometry design for stable finishing of high-hardness materials.
- Key geometry features include:
- • 70% large core diameter for higher rigidity
- • 20° helix angle for stable cutting and smoother machining
- • Negative chamfer edge to strengthen the cutting edge
- • Square end structure for flat-bottom and sharp corner finishing
- • Dedicated CBN grinding process for accurate edge forming
- This structure is designed for finishing and semi-finishing rather than heavy roughing. It is more suitable for stable cutting conditions where edge strength, surface quality, and dimensional accuracy are more important than large material removal.
- Stable Tool Life in Hardened Steel Finishing
- The combination of NL900 CBN material, vacuum brazing, reinforced core design, negative chamfer edge, and precise square end grinding helps improve tool life and batch finishing stability under suitable machining conditions.
- Tool life is affected by workpiece hardness, finishing allowance, cutting parameters, machine rigidity, tool overhang, runout, clamping condition, and toolpath stability. When chipping or rapid wear happens too early, it is often related to unstable cutting conditions, wrong application range, or unsuitable cutting parameters. More details are explained in Why Do CBN End Mills Chip or Wear Quickly? Causes and Solutions
- KERNVEX CBN square end mills are mainly used for precision finishing of HRC60+ hardened steel, quenched steel, and hardened mold materials.
- Suitable workpiece materials include:
- • HRC60+ hardened steel
- • Quenched steel
- • Hardened mold steel
- • High-hardness die steel
- • Heat-treated steel parts
- • Precision mold inserts
- • Flat mold areas and step profiles
- • Small high-hardness precision components
- CBN tool selection should not depend only on the material name. The actual workpiece hardness, finishing allowance, machine rigidity, and surface requirement should also be considered. For more details, see What Hardness Range Is Suitable for a CBN End Mill?
Technical illustrations and dimension data